
01
Material and finish
Provide material, thickness, surface finish and flatness together with any handling limits for the side-standing sheet.
V-Grooving · ADRK Series
Servo-controlled grooving in a compact vertical platform, with multi-tool cutting and pneumatic clamping.
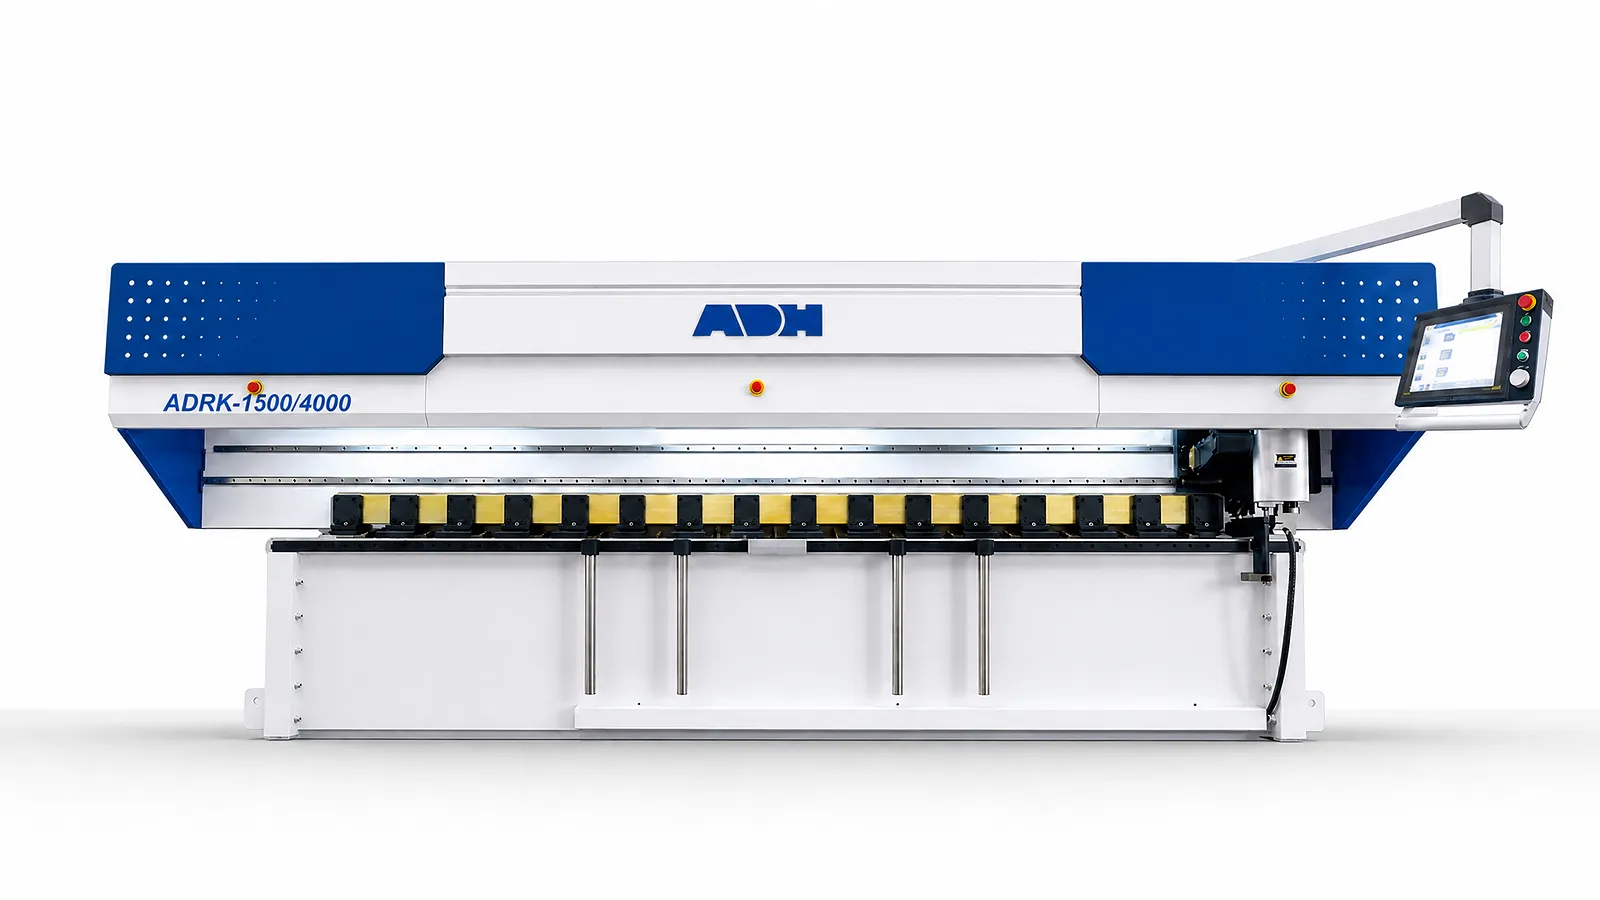
Technical specifications
For the ADRK 3200 × 1250, the main servo motor is rated at 4.4 kW and the hydraulic system operates at 6–8 MPa. Select the row for your sheet size and check the groove depth, edge distance and thickness with a sample of your material.
| Model | Max Grooving Width | Max Grooving Length | Max Sheet Thickness* | Min Sheet Thickness | Min Edge Distance | Max Cutting Speed | Return Speed | Horizontal Resolution | Vertical Resolution | Vertical Positioning Accuracy | Positioning Accuracy | Main Servo Motor | Hydraulic Pressure | Overall Dimensions |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Unit | mm | mm | mm | mm | mm | m/min | m/min | mm | mm | mm | mm | kW | MPa | L×W×H mm |
| 3200*1250 | 1250 | 3200 | 6 | 0.4 | 8 | 0-90 | 0-120 | 0.001 | ± 0.01 | 0.001 | ± 0.01 | 4.4 | 6-8 | 5000*2550*2100 |
| 3200*1500 | 1500 | 3200 | 6 | 0.4 | 8 | 0-90 | 0-120 | 0.001 | ± 0.01 | 0.001 | ± 0.01 | 4.4 | 6-8 | 5000*2800*2100 |
| 4000*1250 | 1250 | 4000 | 6 | 0.4 | 8 | 0-90 | 0-120 | 0.001 | ± 0.01 | 0.001 | ± 0.01 | 4.4 | 6-8 | 5800*2550*2100 |
| 4000*1500 | 1500 | 4000 | 6 | 0.4 | 8 | 0-90 | 0-120 | 0.001 | ± 0.01 | 0.001 | ± 0.01 | 4.4 | 6-8 | 5850*2800*2100 |
Grooving inputs
Vertical orientation changes support and access, but groove geometry, residual thickness and the downstream bend remain the primary inputs.
01
Provide material, thickness, surface finish and flatness together with any handling limits for the side-standing sheet.
02
Define sheet length and width, loading route, support needs, machine envelope and service access.
03
Record depth, angle, residual thickness, direction, edge distance, pass plan and cutter geometry.
04
Confirm batch mix, program storage, chip handling, guarding, light protection, downstream bend and acceptance measurement.
Machine in operation
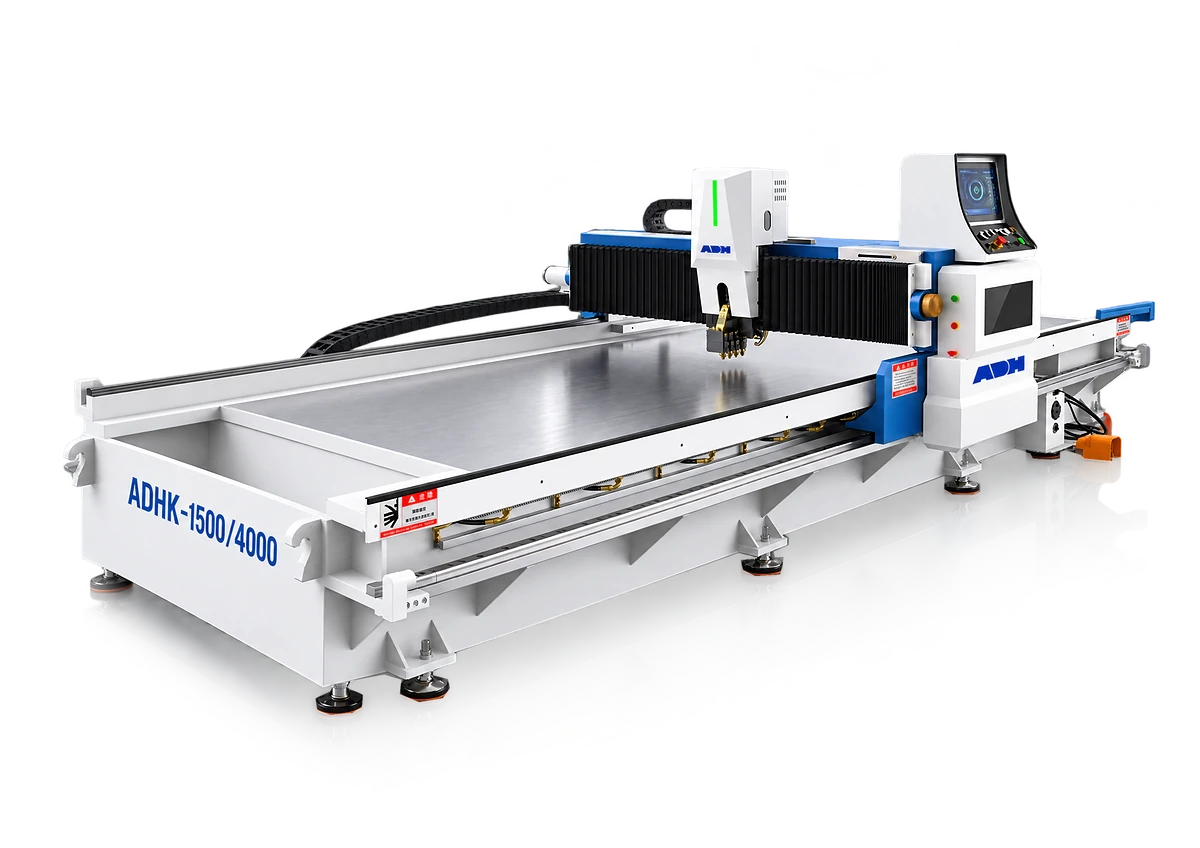
Watch the ADHK-1500/4000 demonstration, then compare sheet positioning, clamping and groove preparation with your material and part drawings.
Watch on YouTube (opens in a new tab)Product systems
ADRK processes a side-standing sheet with programmed positioning and tool motion. Assess support, clamping and access for the actual panel size and finish.
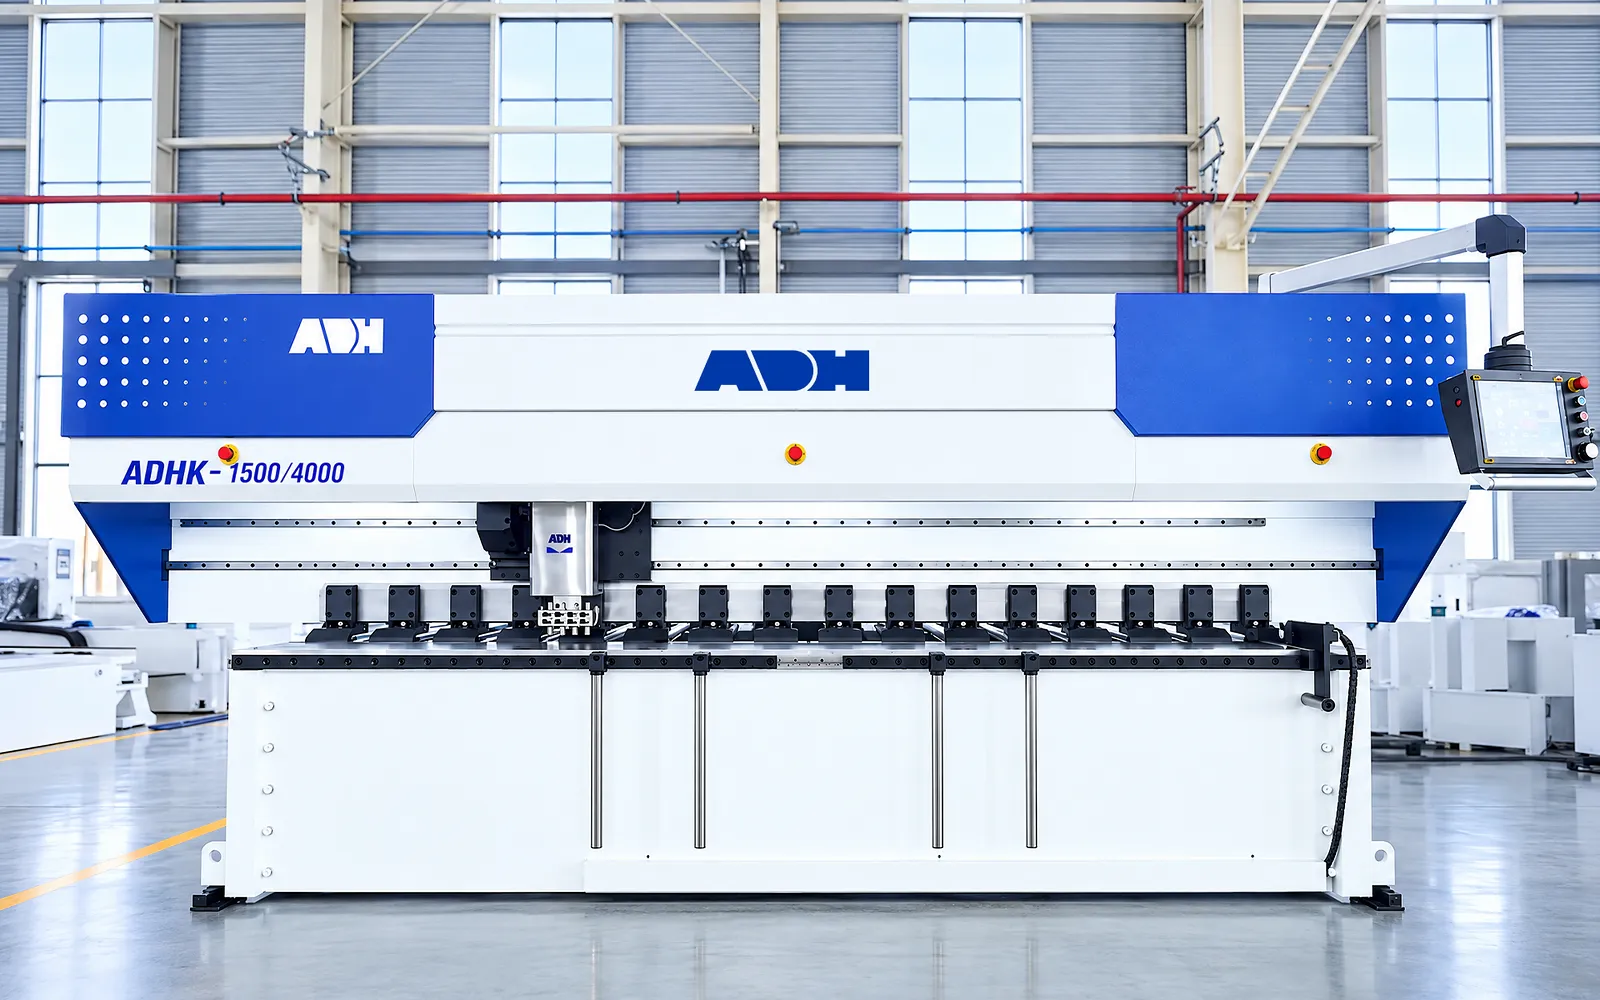
01
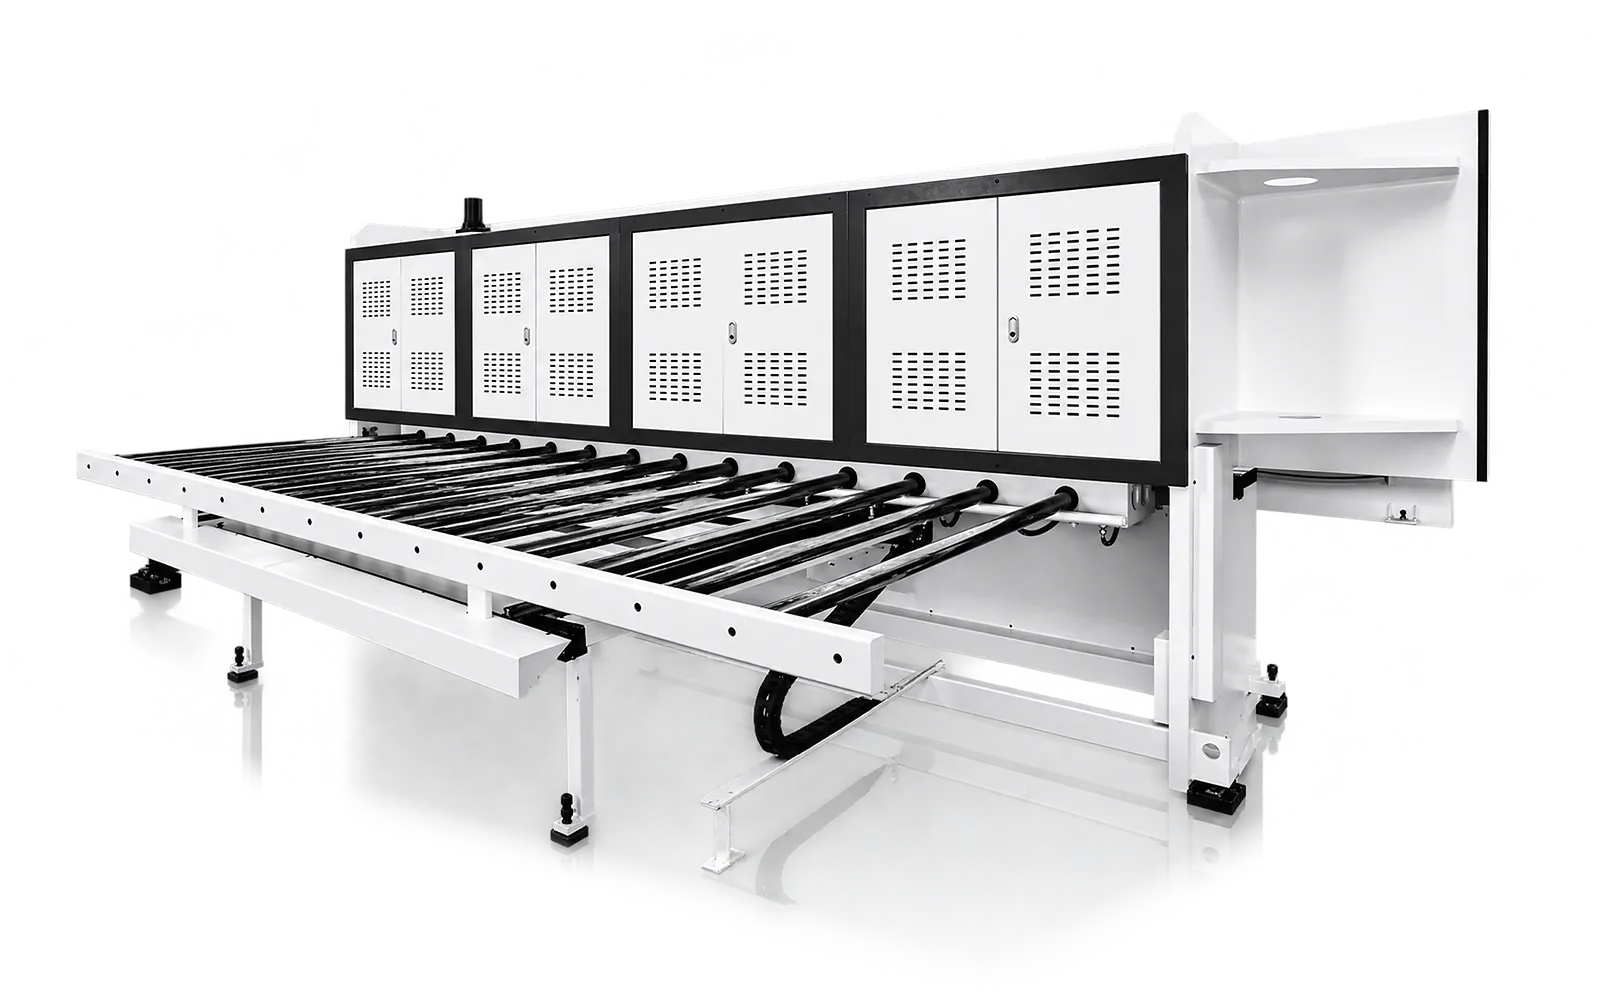
The ADRK arrangement processes the sheet in a side-standing orientation. The frame and supports establish the working reference while allowing access to the panel.
Assess the complete installed footprint, loading method and panel support. Space and handling needs depend on the actual sheet format.
Backgauge
The backgauge establishes the programmed groove position.
Review the required groove positions and sheet reference on representative panels.
Clamping
Distributed pneumatic clamping maintains the sheet reference during grooving.
Review flatness, contact points and clamping zones. Check cleaning access and possible surface marking.
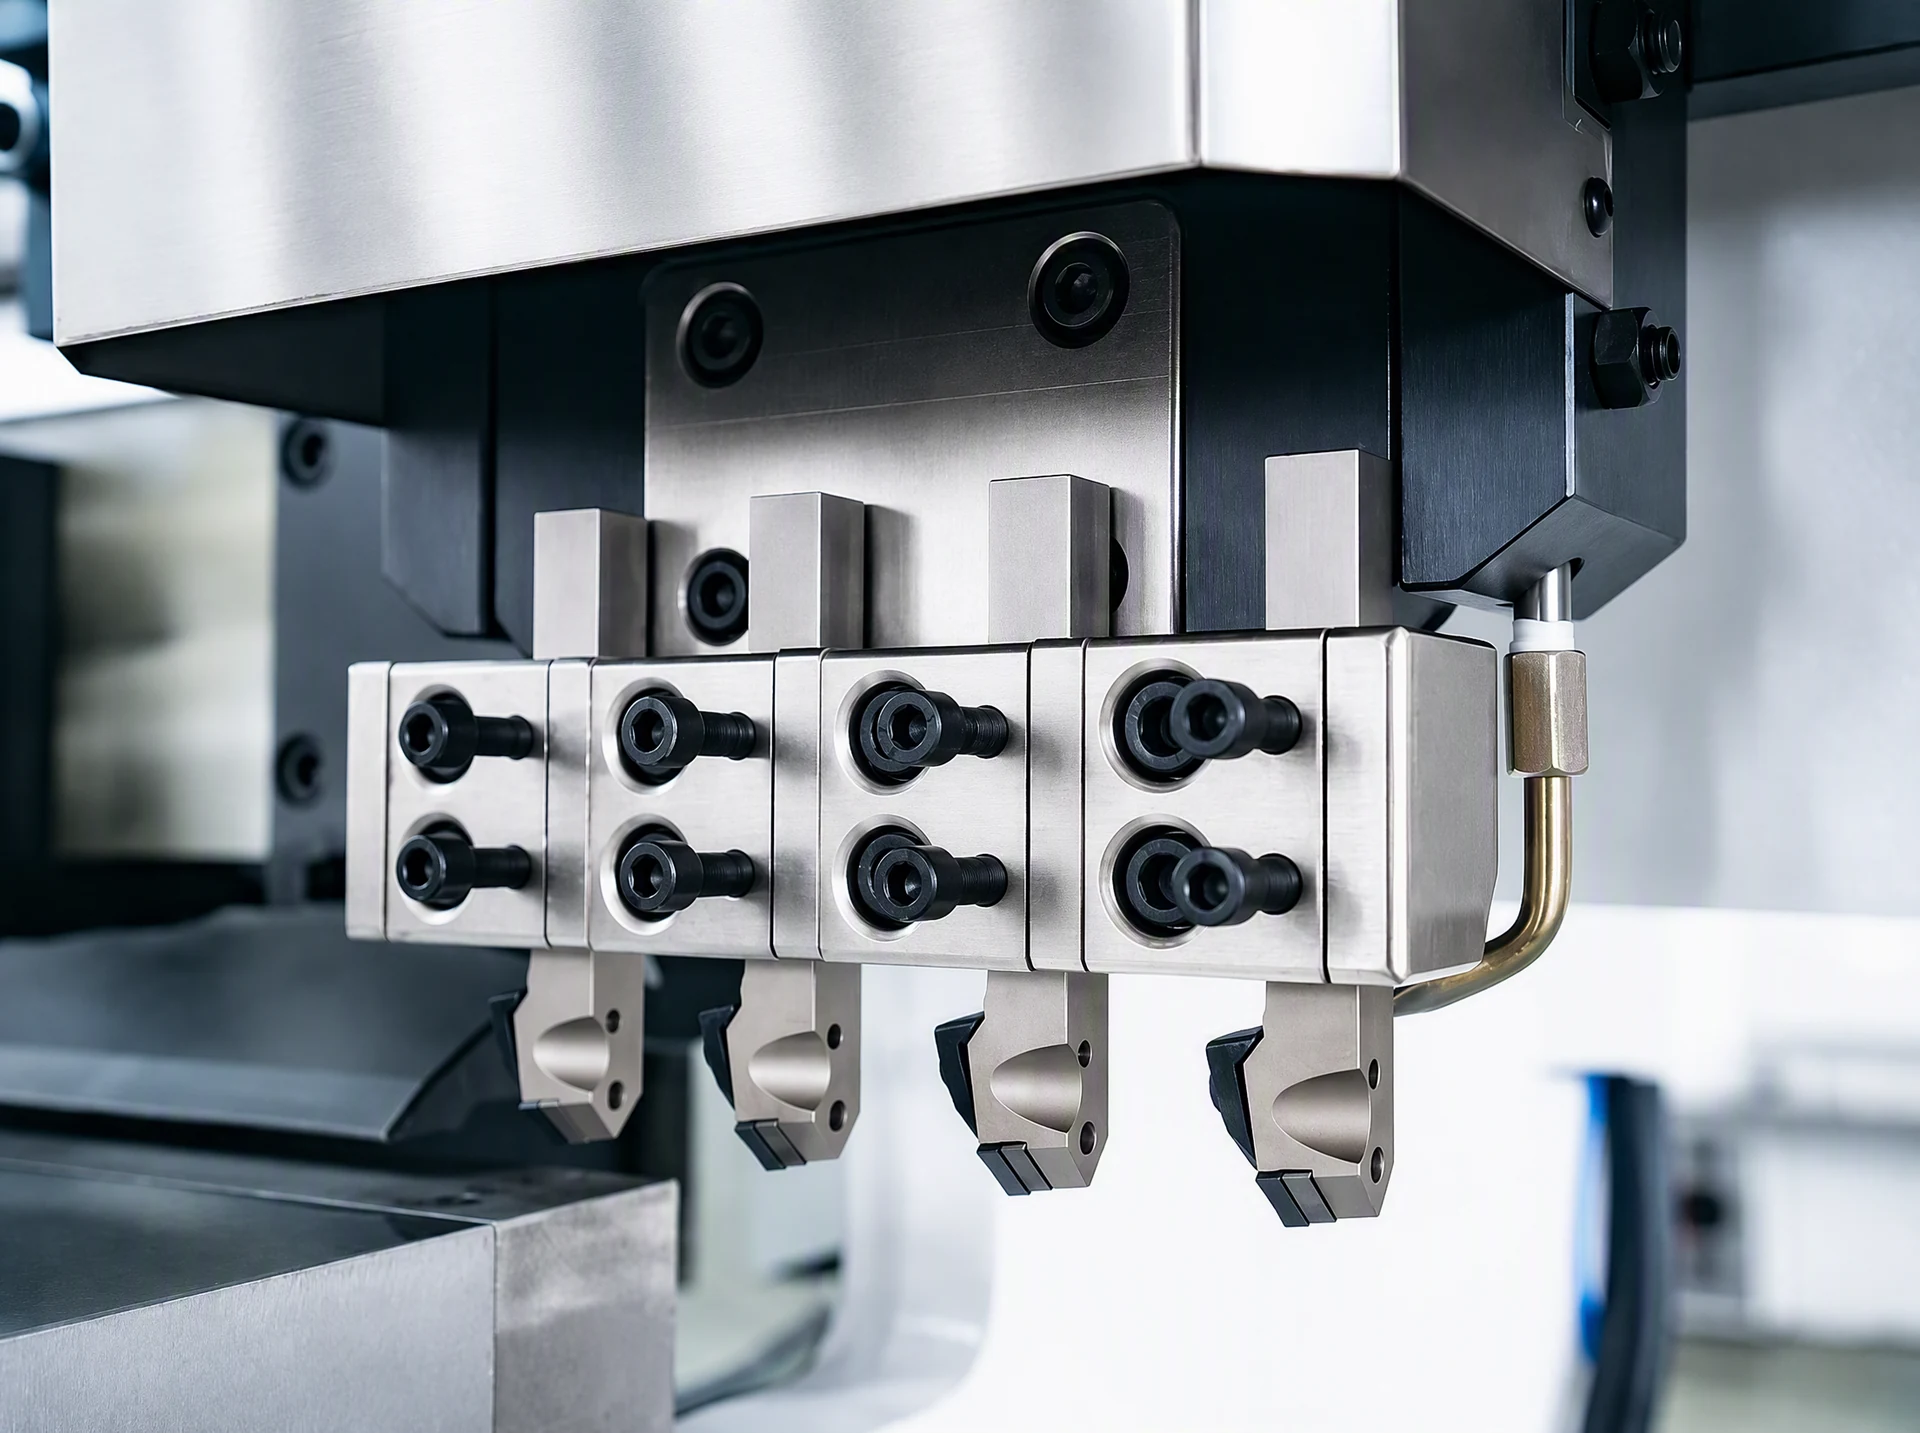
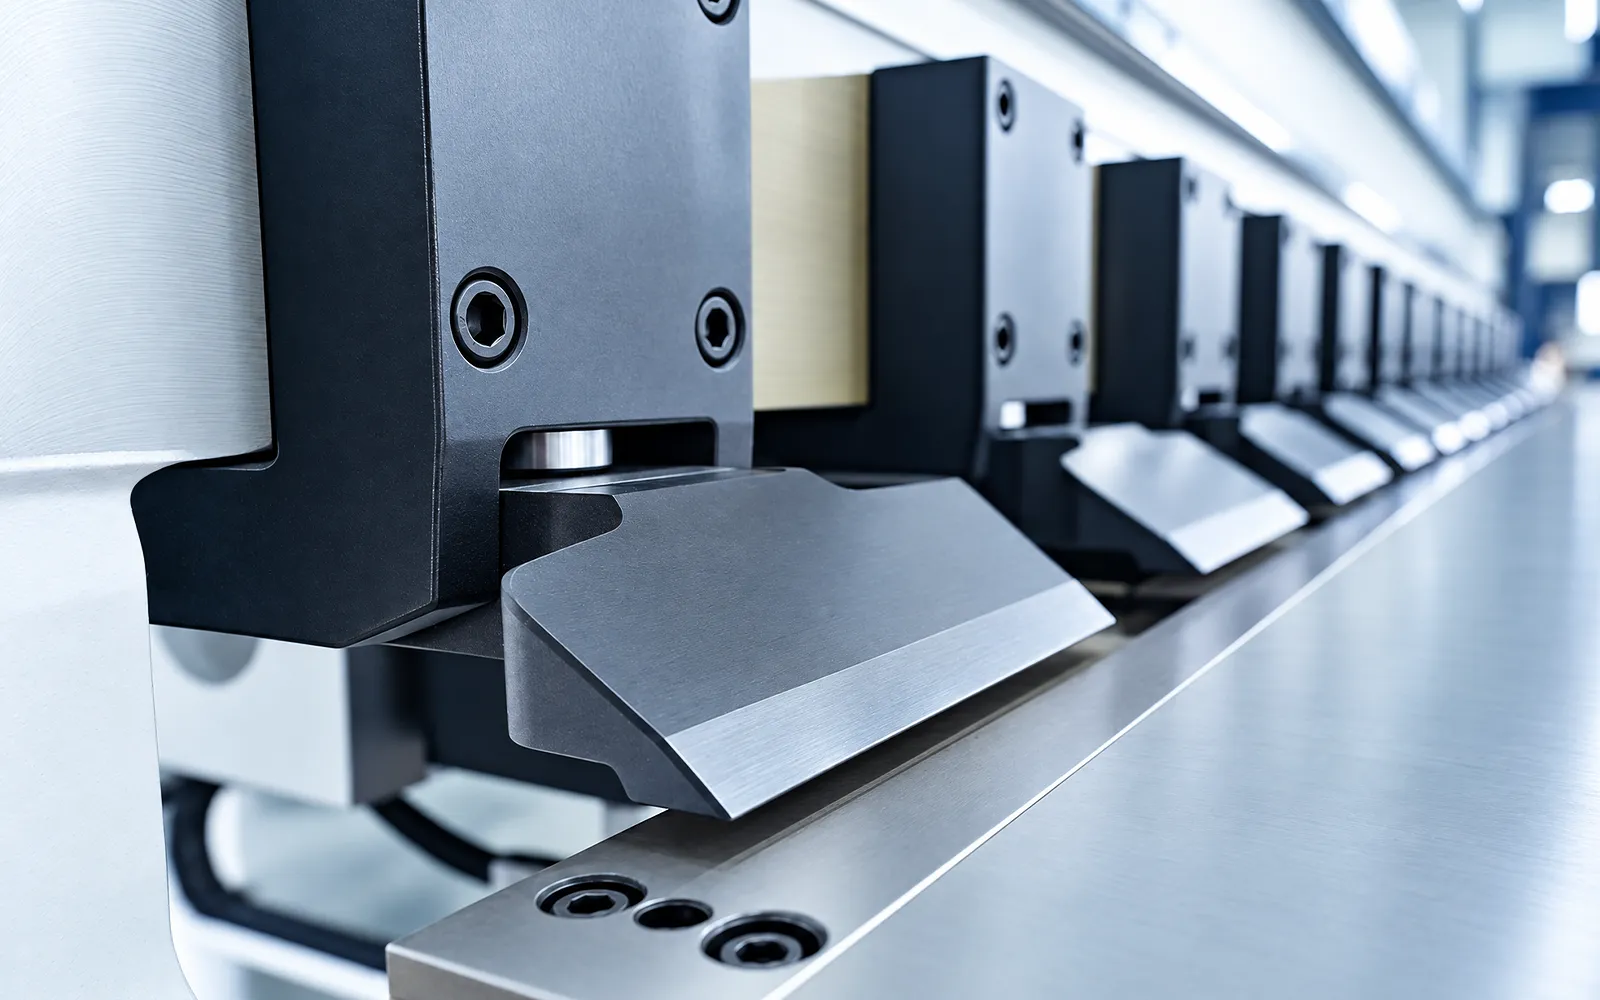
03
The documented arrangement uses four tools in a progressive sequence. Cutter geometry, condition and the selected passes determine the groove form and remaining thickness.
Six-tool or special-groove arrangements require a defined configuration. Feed and return speeds describe machine motion, not the complete job time.
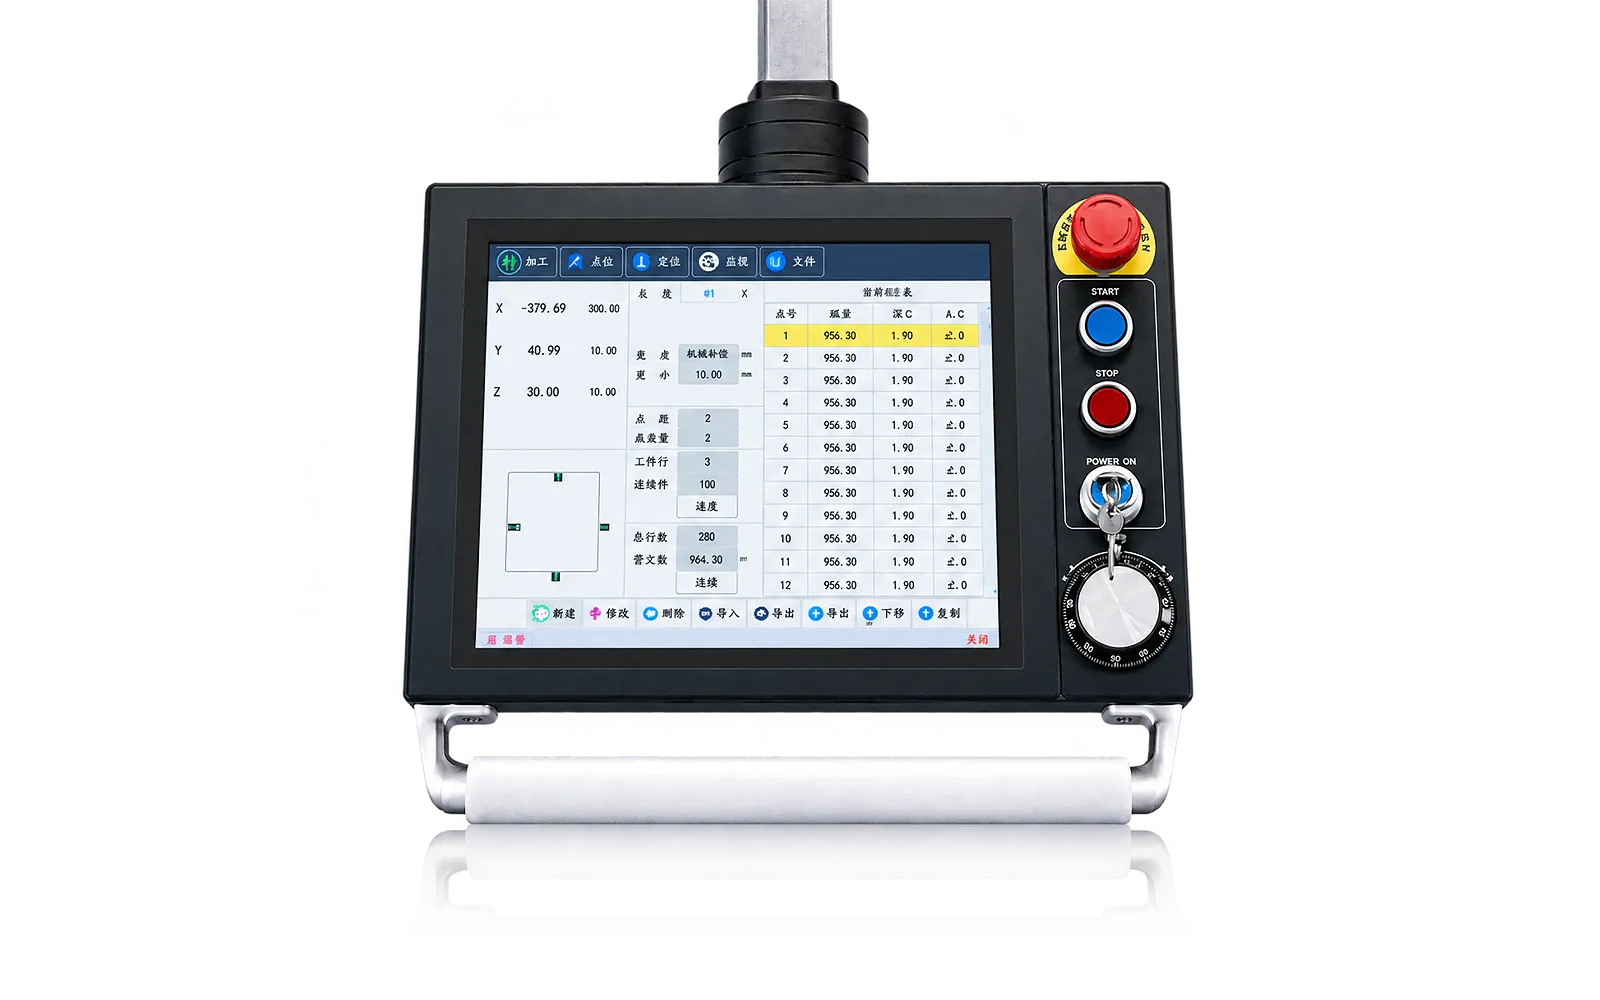
Servo control
The program defines groove positions and depth while servo axes coordinate travel and tool motion.
Review diagnostics, limits and pressure or load monitoring. External-data and robot connections depend on the ordered system.
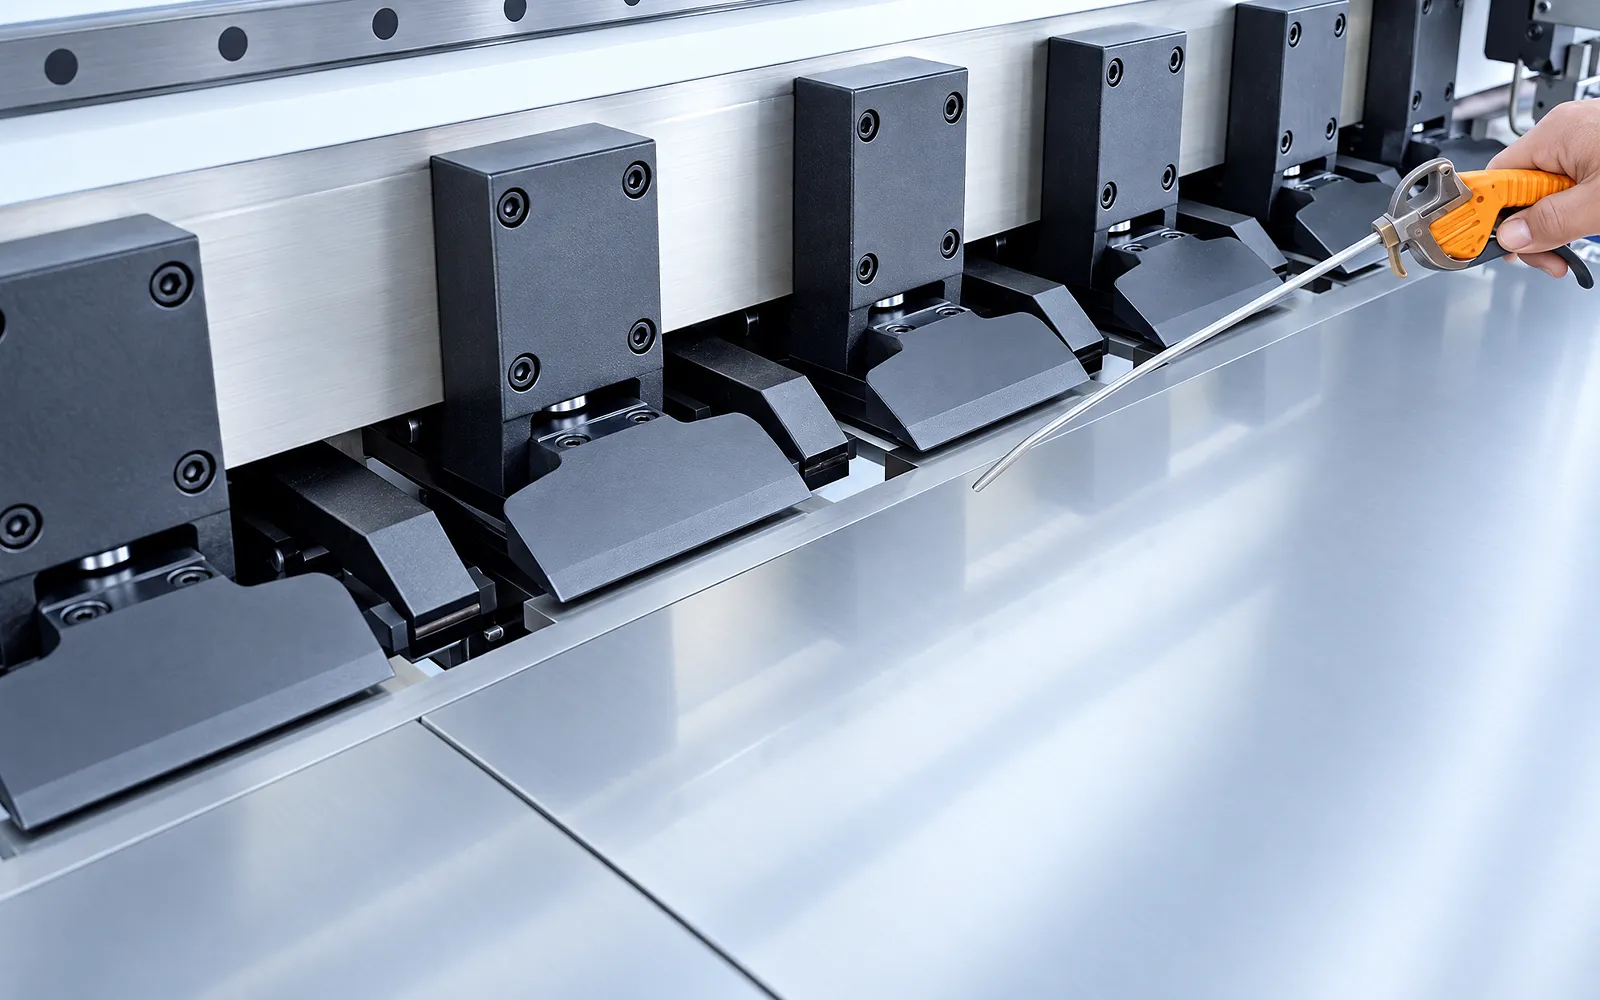
Operating access
Operating access must accommodate tool work and chip cleanup around the panel.
Review service and cleanup positions together with the intended panel-handling route.
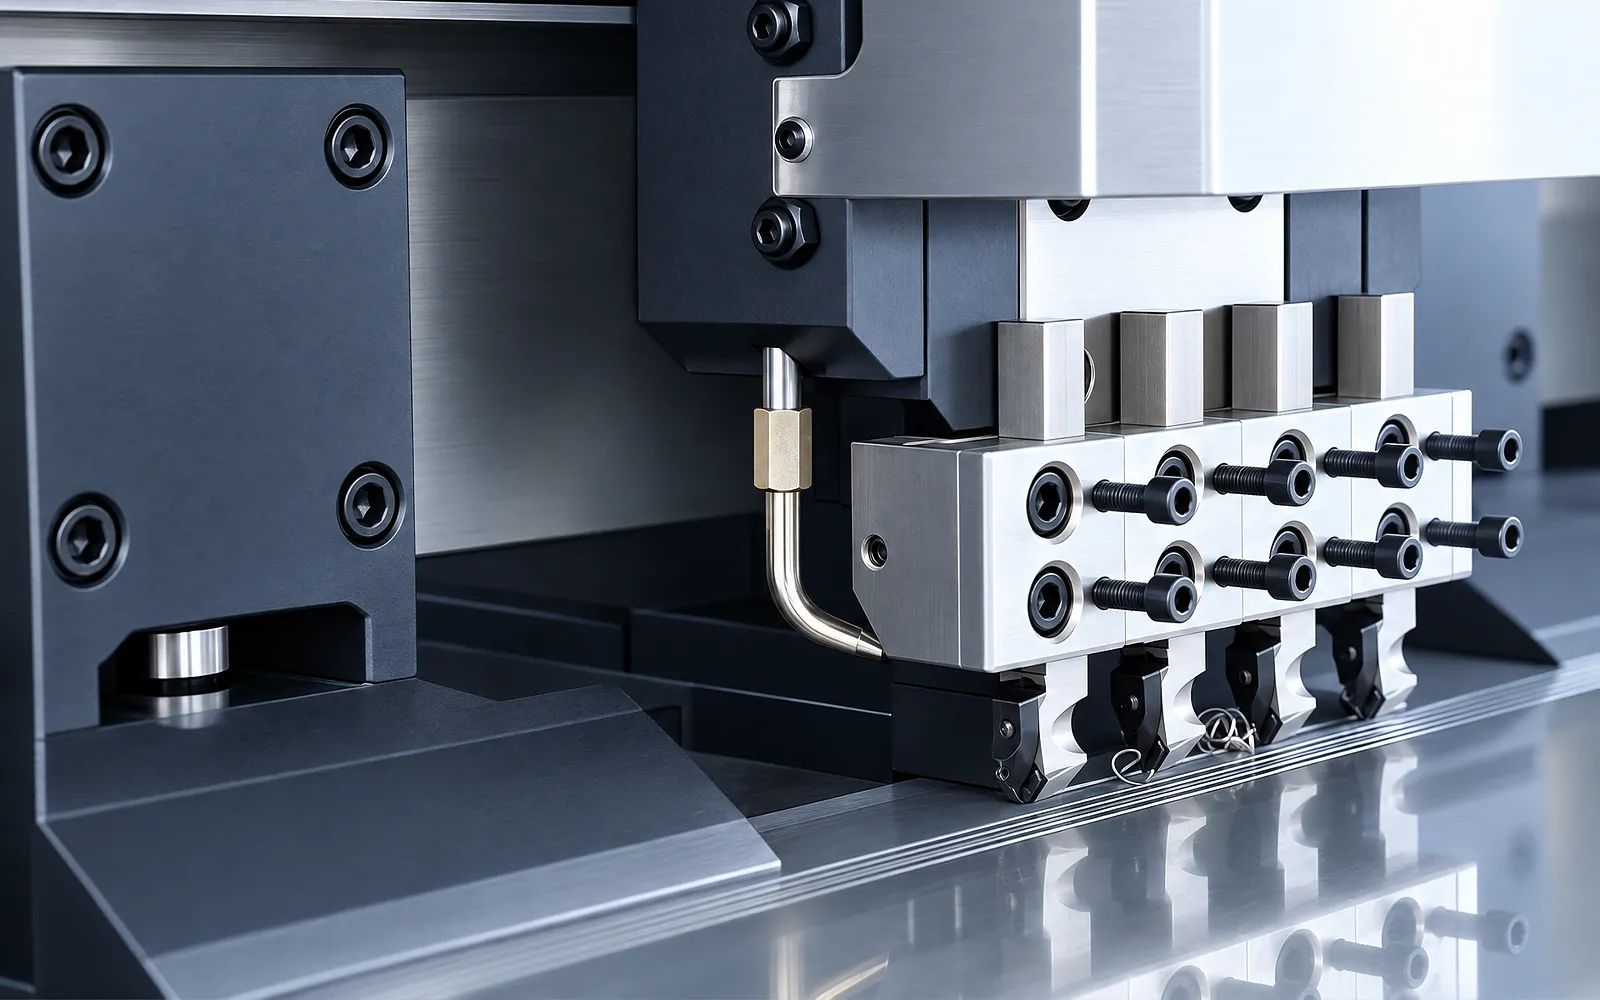
Panel trial
A representative panel tests support, clamping, tool sequence and depth control.
Inspect groove geometry and remaining thickness using the agreed material, finish and drawing.
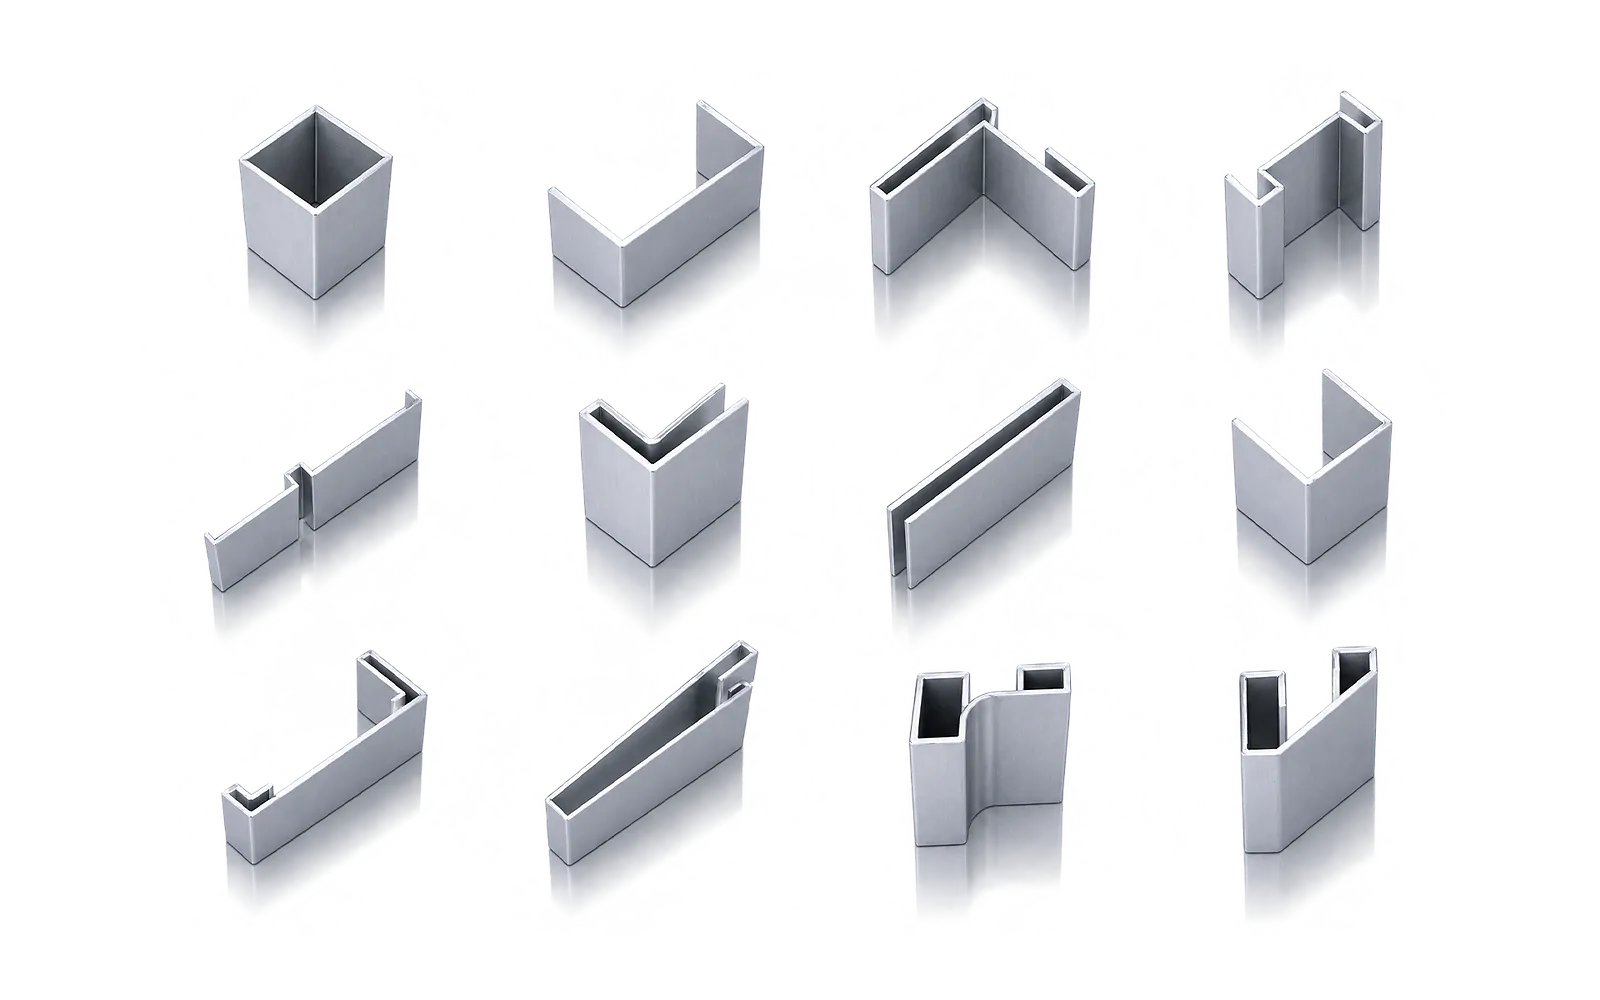
Formed-corner trial
Inspect the formed corner after bending the prepared panel.
Define inspection points and the acceptable corner and surface result before sample review.
Specification boundary
Use the selected ADRK model row for motor, dimensions and motion values; confirm any optional arrangement.
Use the exact ADRK model data for the selected size, including 4.4 kW motor values and listed dimensions.
Special grooves, six tools, light protection, loading, chip collection, MES and robot interfaces require confirmation.
Confirm sheet support and finish, groove geometry, pass plan, residual thickness, tool criteria and downstream bend acceptance.
Related machines & selection
Through the machine lifecycle
Find the training, maintenance guidance and parts support your team needs. Services and availability are confirmed for your machine and location.
Before start-up
Prepare utilities, lifting and the installation area, then coordinate start-up and handover.
Review installation supportBefore production
Build the operator, programming and maintenance skills required for your delivered machine.
Explore trainingIn operation
Get support with the machine model, serial number and a clear description of the issue.
Request technical supportPlanned spares
Identify your machine and component so our team can check compatibility and availability.
Request service or partsSelf-service
Find video guidance for operating and maintaining your ADH machine. Check relevance to your model and configuration.
Browse support videosContract scope
Your quotation or contract defines included services, warranty, exclusions and responsibilities.
Review service scopeProject enquiry
Tell us what you want to make or improve. Technical details and drawings can follow.
Contact ADH
Name, email and a short description are enough to begin.